Customer Success Stories
Serving industry-leading enterprises, delivering value through expertise.
Powder Raw Material Impurity Removal and Sieving Project in the Chemical Industry
Configure the S49-A rotary sieve and powder screening system to safely screen and purify chemical raw material powders, intercept foreign matter and coarse particles, and ensure stable downstream production processes.
Chemical powder raw materials often contain foreign matter and coarse particles. If introduced directly into downstream processes, they compromise product purity and production continuity. Manual inspection is inefficient, and controlling dust on-site is challenging.
System operates continuously and stably, effectively removing foreign matter and coarse particles. Powder quality improves significantly, manual inspection workload decreases, and the on-site environment becomes cleaner.
Corn starch screening and conveying project for a biotech company in Jiangsu
Customized Dust-Free Feeding Station + Vacuum Conveyor + Vibrating Sieve Solution for Corn Starch Pre-Screening, De-Lumping & Foreign Material Removal, and Closed-Dust Transfer
Manual feeding causes dust clouds and poor workshop conditions. Starch tends to clump and may contain foreign matter, compromising product quality. Manual feeding also imposes high physical labor demands.
The entire system runs continuously and stably, completely eliminating workshop dust issues. Labor costs are reduced by 65%, production capacity is consistently maintained at 2000-3000 kg/h, and the finished product pass rate has significantly improved.

Mining Company Screening Production Line
Heavy-duty vibrating screen + feeder complete screening system with integrated dust collection and noise reduction equipment
Hard ore with severe abrasion demands extremely high equipment strength and wear resistance.
Screening efficiency exceeds 95%, equipment lifespan extended by 2 times, and labor costs reduced by 60%
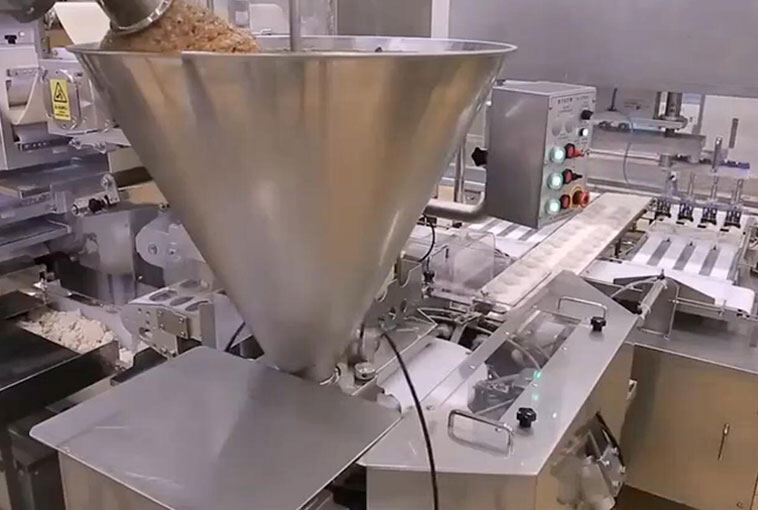
A Food Company in Nanjing
LS-450/550 Filter Sieve and S49-800 Vibratory Sieve, compliant with GMP hygiene standards
As society advances and living standards rise, public expectations for food safety and hygiene continue to grow. Leading food companies are now controlling safety at the source of production. Before flour enters the mixer, it must undergo protective sieving to prevent foreign contaminants from entering downstream processes, thereby avoiding food safety issues and consumer complaints.
Capacity: 500-2000 kg/h Mesh Size: 20 mesh (Aperture: 0.85mm) Equipment Application Flow: Bagged Flour → Bag Opening → Manual Feeding → Vibrating Screen & Filter Screen → Transfer Drum → Dough Mixer & Blender
Food Flour Impurity Removal and Sieving Project in Nanjing
Configure GFDZ dual-vibration linear screen, S49-A rotary vibrating screen, and flour sifting system to perform 40-mesh safety screening before flour enters the mixing process. Capacity: 1 tons/hour. Prevent foreign matter intrusion and ensure food production safety.
Raw powder is prone to foreign matter contamination. If it enters downstream processing, it poses food safety risks and may trigger customer complaints.
Ensures continuous, stable operation by effectively filtering raw material impurities. Controls food safety at the source, meets hygiene standards, and guarantees end-product quality.

Material Feeding System Retrofit for Pharmaceutical Enterprise
Vacuum Conveyor + Manual Loading Station Combo for Enclosed Automated Feeding
Powdered drugs are prone to dusting and cross-contamination; compliance with GMP certification is required.
Achieve zero dust leakage, GMP certified, and reduce labor input by 50%.

Coal Conveying System Project for a Power Plant
Large-incline Belt Conveyor + Magnetic Separator + Electronic Scale for Precise Coal Conveying and Metering
Long transport distances and significant elevation changes require measures to prevent material sliding and spillage.
Conveys up to 800 meters with stable operation and measurement accuracy of ±0.5%
Fine Screening Project for Powder Raw Materials at a Printing Technology Company in Anhui
Custom Dust-Free Loading Station + S49-A Vibrating Sieve Solution for precision screening of printed auxiliary materials after drying and before packaging, with 200 / 325 mesh grading and purification to ensure powder cleanliness.
Fine powders easily blind screens, making continuous operation impossible with standard sieving equipment. Contaminants compromise product quality, requiring strict material cleanliness controls.
The device supports 24 hours of continuous stable operation. Ultrasonic cleaning eliminates mesh clogging, and the absence of cleaning balls still meets cleanliness requirements. Screening efficiency is significantly improved, ensuring consistent product quality that meets specifications.
Similar needs? Contact us
Professional team offers free technical consulting and customized solutions.
Get Started